This guide helps you evaluate supplier fit, pricing logic, and quality risk when sourcing industrial components using the identifier 33998412549. Objectively, it explains what supplier selection involves, how cost structures typically form in procurement, and what documentation and inspection processes reduce uncertainty. You’ll also find decision conditions and FAQs to support consistent buying near-by.
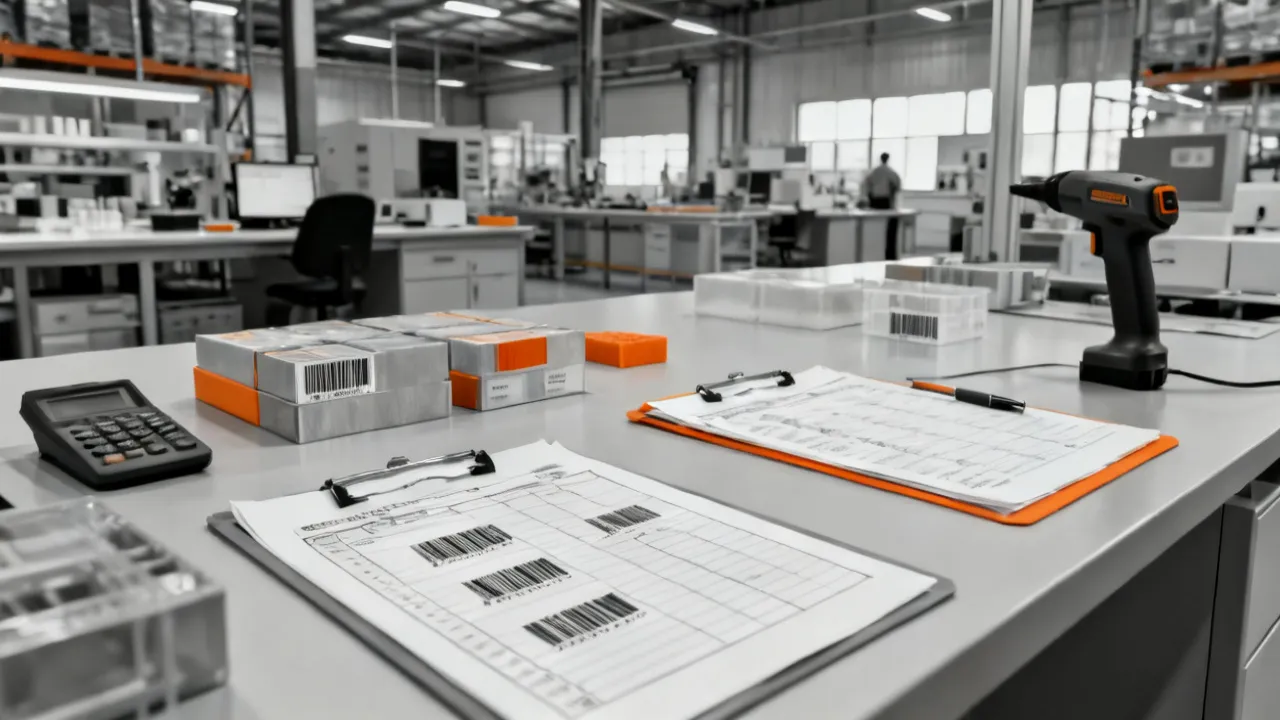
If you are sourcing industrial parts tied to the identifier 33998412549, the very important step is to confirm that the supplier’s capability, quality systems, and pricing structure match your real requirements—then document acceptance criteria up front. This is where procurement decisions succeed or fail: not at the moment of payment, but at the moment you define what “good” means.
In practical procurement work, “price” rarely represents the entire cost of ownership. For industrial components, the effective cost is shaped by lead time reliability, inspection acceptance rates, packaging integrity, traceability, and the likelihood that parts will meet dimensional and material specifications on the first build cycle. The goal of this article is to support an objective evaluation approach so you can source more confidently, particularly when you must coordinate multiple stakeholders such as engineering, quality assurance, warehouse receiving, and finance.
When done well, this approach does more than prevent obvious defects. It prevents hidden failure modes such as documentation mismatches, incomplete certifications, incorrect revision control, sub-supplier changes that alter material properties, and packaging practices that create receiving delays. Those issues frequently originate at the procurement stage—before production even begins—so the “real” purchase decision is effectively the documentation and requirements lock-in you set at quotation time.
The identifier 33998412549 is top treated as a reference key inside a sourcing or inventory system—often connected to a part record, a lot/traceability entry, or an internal SKU-like mapping. In many organizations, these identifiers allow procurement teams to cross-check drawings, material certifications, test reports, and historical supplier performance. Even when the identifier appears only as a number, it usually implies that documentation exists somewhere in your supply chain records.
Expert lens: From an industry perspective, the number itself is less important than the data behind it. A robust supplier should be able to answer: What exact part revision does this refer to? What certifications apply (e.g., material certificates, compliance statements, inspection reports)? What tolerances and test methods are relevant? A supplier who cannot quickly tie 33998412549 to its technical record increases your downstream risk.
In many procurement processes, the identifier is used to ensure that the quote maps to a specific configuration rather than a generic description. For example, a parts list may reference 33998412549 while engineering holds a drawing set that includes revision history, alternate materials, and specific process notes (heat treat, surface treatment, finishing roughness, hardness range, or inspection method). If the supplier quotes against an outdated revision, the parts can physically resemble the target but fail functional validation. That is why the procurement stage must establish what revision/record is required and how that will be confirmed on delivery.
There is also a practical reason identifiers matter for traceability: many regulated or auditable environments require a paper trail from raw materials through manufacturing to final inspection. If your receiving team cannot reconcile delivery documentation to 33998412549, you may hold inventory—even if the parts appear to be in-spec visually. The result is expensive “soft rejection”: parts occupy space and stall assembly while the documentation gap is resolved.
When buyers see inconsistent quotes—sometimes even for the same nominal part—they are usually observing differences in how suppliers price uncertainty and requirements. In objective procurement terms, industrial pricing can be influenced by:
Because these cost drivers are often interdependent, a “lower price” quote may contain hidden trade-offs—such as reduced inspection scope or less robust packaging—which can increase your total cost later. Therefore, comparing suppliers should focus on the full quote basis: what is included, what is excluded, and under what acceptance conditions.
To expand on this, consider that suppliers typically price not only the manufacturing time but also the compliance work required to close the loop between raw materials and your receiving requirements. If you request that 33998412549 be delivered with a complete certificate packet and labeled traceability, the supplier must capture and assemble documentation. That may require additional internal handling steps (document generation, review, approvals, and sometimes sub-supplier paperwork retrieval). Suppliers often reflect those administrative costs implicitly inside the unit price unless you force a transparent breakdown.
Additionally, inspection intensity changes cost more than buyers sometimes expect. For example, dimensional inspection can require calibrated tools, measurement staff time, and defined sampling procedures. If the supplier proposes a cheaper inspection plan—such as a lower sampling frequency or less stringent method—your risk of nonconformance increases. That risk can manifest as rework, scrapped assemblies, line stoppages, or extra incoming inspection workload for your team.
Lead time pricing is another frequent source of mismatch. A supplier might quote a longer lead time at a lower unit rate because it can schedule production on a stable plan with fewer expediting costs. If you need a shorter delivery window, they may “rush” the operation, causing overtime, priority queue changes, or reallocation of machines and quality resources. The resulting quote difference is not just schedule-related; it can also correlate with increased variability in processing and documentation flow if the supplier is operating under pressure.
Finally, packaging and handling costs are sometimes underestimated. In high-mix industrial environments, packaging errors cause receiving delays: labels may be unreadable, documentation may be separated from parts, parts may arrive without protective protection appropriate for your receiving environment, or packaging may not meet your warehouse handling standards. Those issues typically generate extra labor for quarantine, repack, relabel, or coordinate with the supplier. Over time, the “true cost” of poor packaging becomes visible through operational friction.
Choosing a supplier near-by or in any region with your logistics network should be evaluated using consistent criteria rather than convenience alone. A disciplined supplier assessment typically covers three layers:
Industry expert viewpoint: In many manufacturing supply chains, the “paper quality” of certifications matters less than the supplier’s ability to produce consistent results across batches. That consistency is usually visible through robust internal controls: calibration, process validation, effective corrective action, and clear traceability from raw material to finished goods.
To make this concrete, a supplier evaluation should address both “can they build one good part” and “can they repeatedly build good parts while maintaining documentation integrity.” For parts tied to 33998412549, the second part is often more challenging: documentation and traceability must remain consistent from lot to lot, not only manufacturing outputs. If a supplier’s process quality depends on individuals (e.g., one particular reviewer generates certificates correctly), you may experience inconsistent documentation performance during personnel changes, subcontractor switches, or production surges.
Quality system maturity should include the supplier’s ability to control revisions and changes. A common risk occurs when a supplier implements a process improvement or substitutes a material source. Even if the end result is near the original spec, you may need formal change notification for your compliance and configuration control. A mature supplier will have documented change control workflows and will communicate changes before they affect your production usage. Without this, the buyer’s procurement team must rely on reactive communication when parts arrive with documentation that no longer matches the drawing or record behind 33998412549.
Evidence of performance should be evaluated using measurable indicators. Instead of relying on “we have good quality,” ask for metrics such as incoming inspection pass rates in previous business, on-time delivery performance (OTD), number of nonconformances per shipment, average containment time, and the supplier’s average corrective action closure cycle. If you are qualifying a supplier new to your organization, ask for references or anonymized performance summaries tied to similar parts in similar material systems or tolerances.
It is also valuable to ask how the supplier manages sub-suppliers. Many industrial parts are assemblies of processes performed across multiple vendors: casting or forging, machining, heat treatment, surface finishing, plating or coating, and final inspection. If your chosen supplier does not own those upstream controls, they may deliver incomplete traceability. A good supplier will either perform those processes in-house or maintain robust governance of sub-suppliers with documented receipt controls and traceability bridging.
For higher-criticality parts, your evaluation might include requesting a capability statement that demonstrates measurement system adequacy (e.g., gauge calibration status, MSA approach where applicable, or measurement uncertainty considerations). Even if you do not require formal statistical capability indices, you should still confirm how measurement and inspection methods are defined and controlled.
To make pricing comparisons meaningful, compare quotes on a like-for-like basis. The very effective approach is to attach a “quote scope checklist” to each supplier response. Your procurement team can then confirm that each supplier includes the same deliverables (e.g., inspection reports, labeling, packaging level, revision control references, and any compliance statements relevant to your application).
Where the identifier 33998412549 is used, ensure each supplier quote references the correct revision or record. If revisions differ—even slightly—the part may fit physically yet fail functional tests due to material or process changes.
Scope checklisting prevents a common procurement failure mode: vendors intentionally or unintentionally quote different “packages.” One supplier may include a complete certificate packet and full dimensional inspection. Another supplier might provide only a basic certificate of conformity with no detailed inspection data. Both can present a competitive unit price, but only one includes the evidence required for your internal verification.
Acceptance criteria should also be clarified. For example, drawing-based tolerances may define ranges for dimensions, hardness, surface roughness, coating thickness, or other functional characteristics. However, acceptance criteria also include “how” those characteristics are measured, not just the final allowed range. Two suppliers might both claim compliance, but if they measure with different methods or sample sizes, their probability of meeting your true requirements changes.
Procurement should therefore require that suppliers specify:
When suppliers understand you are comparing like-for-like, they are more likely to quote the true cost of meeting your acceptance requirements. That transparency reduces future disputes and supports more stable supplier relationships.
Even when you source from “nearby” regions (replacing any city/country placeholders with “nearby” as required), operational realities remain similar: warehouses need predictable receiving, quality teams need clear documentation, and production schedules need stable lead times.
Local logistics can reduce some friction—such as shorter shipping windows and easier coordination for urgent deliveries—but it does not eliminate risk. A supplier “nearby” may still deliver inconsistent documentation, or parts may arrive with insufficient labeling for your traceability process. Therefore, local proximity should be treated as a potential advantage, not a substitute for verification.
When sourcing nearby, you can often improve speed of communication for resolution if nonconformance occurs. However, you still need well-defined pre-receiving rules. For instance, if your receiving team has a checklist requiring that certificates include a specific revision identifier, a specific lot/heat number mapping, and specific labels that reference 33998412549, you must enforce that checklist consistently regardless of shipping distance.
Also consider the risk of assumptions. Many procurement teams assume that local suppliers are easier to qualify because they “should be” responsive. But responsiveness does not guarantee technical compliance. A supplier might be fast at answering emails yet still have quality gaps in calibration control, sampling plans, or traceability labeling. Therefore, local sourcing should not replace supplier evaluation and evidence collection; it should only reduce logistical delay for communication and correction.
In some organizations, nearby sourcing introduces additional operational benefits: you may be able to schedule pre-shipment inspections, arrange faster audits, or run sampling-based verification upon arrival. If your schedule allows, consider adding a pre-shipment verification step for first-article shipments tied to 33998412549. That step can be especially valuable when you are qualifying a new supplier or when you suspect that revision control and traceability might vary.
From a manufacturing operations standpoint, the costliest sourcing failures are the ones discovered late. The strongest mitigation measures are:
These practices help ensure the number 33998412549 corresponds to a stable and verifiable record in your system, rather than an ambiguous part entry.
To expand on risk management, it helps to categorize risk into at least four types:
Risk mitigation measures should address all four. For specification risk, PPR and agreed inspection methods reduce ambiguity. For documentation risk, traceability labeling and certificate package checks at receiving prevent “paper gaps.” For operational risk, lead time verification and delivery reliability metrics reduce schedule disruption. For systemic risk, quality system evaluation and structured corrective action reduce recurrence.
Corrective action escalation is particularly important. Many suppliers respond to nonconformance with quick containment but limited root cause analysis. A strong corrective action workflow should include: containment actions (quarantine lots, block shipment if needed), root cause analysis, corrective actions to prevent recurrence, verification of effectiveness (often through re-inspection and review of subsequent lots), and closure evidence. Your procurement team should not treat corrective action as an optional process; it is the mechanism by which the supplier earns continued business.
Also consider that not all nonconformance is obvious at first glance. Some parts can appear acceptable visually yet fail due to hardness range, microstructure, coating thickness, or internal defects. This is why agreed inspection methods matter. If the supplier uses a test method that is not equivalent to your acceptance method, the probability of passing your internal verification changes. That is another reason to define acceptance criteria in the quote scope rather than leaving it to interpretation.
The table below summarizes common procurement conditions you can use to compare suppliers for an industrial part reference such as 33998412549. Use it as an internal rubric—then require evidence during quoting.
| Evaluation Area | What to Require | Evidence to Ask For | Typical Impact on Total Cost |
|---|---|---|---|
| Technical Match | Correct part revision, drawing compliance, and dimensional tolerances | Revision-controlled drawing acknowledgment, measurement approach | Reduces rework and assembly failures |
| Material & Process Traceability | Traceability from raw material to finished goods | Material certificates, batch/lot mapping, labeling samples | Improves audit readiness and reduces downstream risk |
| Inspection & Test Methods | Defined inspection plan and acceptance criteria | Inspection procedures, calibration records, method references | Influences yield and variability costs |
| Quality System | Process control and documented quality management | Audit reports, corrective action workflow description | Impacts defect rates and response speed |
| Packaging & Handling | Protection appropriate for your receiving and storage conditions | Packaging spec, label layout mock-up, damage history if available | Prevents transit damage and receiving holds |
| Delivery Reliability | Lead time commitments consistent with scheduling needs | Historical lead time performance summary (with method), capacity notes | Reduces line stoppages and expediting costs |
| Documentation Completeness | Included paperwork and revision references | Example certificate packet, packing list format, labeling requirements | Minimizes receiving delays and compliance gaps |
To make this rubric even more actionable, consider adding a scoring dimension. For example:
This way, you can avoid the trap where a supplier looks cheaper but fails high-impact requirements that would trigger line stoppages or expensive rework.
Below is a practical guide you can use internally when selecting a supplier and comparing pricing for industrial components tied to 33998412549.
Before requesting quotes, validate what 33998412549 maps to in your system: drawing revision, material spec, and any application notes. If you have multiple revisions across time, explicitly specify the version you want suppliers to quote against.
In a mature procurement workflow, you also confirm whether your internal record includes alternate materials or process options. For instance, drawings might permit multiple alloys under certain compliance rules, or they might permit two finishing methods with equivalency criteria. If alternatives exist, decide whether suppliers are allowed to use any alternate or whether they must quote a single approved route. Ambiguity here can cause later disputes: the parts may meet broad requirements but fail a narrower functional criterion that your assembly depends on.
Finally, confirm whether 33998412549 represents a specific configuration requiring unique labeling or packaging. Many systems use identifiers to drive label templates and warehouse scanning. If you mis-specify labeling requirements, you can create receiving delays even when parts are otherwise correct.
Send a quote request that includes required deliverables: inspection reports, certificates, labeling format, and packaging requirements. Ask suppliers to confirm in writing that they will include these items.
More specifically, your quote request should distinguish between:
If you omit these categories, suppliers will often infer what you need based on typical practice, which may not match your internal system. A strong procurement request reduces interpretation and reduces risk.
Request objective documentation samples where possible: prior test report formats, certificate packet examples, and a description of how traceability is maintained. If a supplier cannot provide representative documents, treat it as a qualification gap.
When suppliers claim they can meet your requirements, you should still probe how. Evidence requests can include:
In some cases, you can request pre-shipment photos or a label printout mock-up. This can reveal practical issues such as label placement, readability, language requirements, barcodes, and whether labels reference the correct identifier 33998412549 and revision.
For higher-risk parts, request a pre-production sample or first article inspection package aligned to your acceptance criteria. The sample should not be treated as “just a sample”; it should be treated as a formal verification event with documented acceptance.
Separate quote lines into cost drivers: base manufacturing cost, finishing/processing steps, documentation package, inspection scope, and logistics. When quotes are structured differently, normalize them so you compare scope rather than only total numbers.
A practical normalization method is to create a “quote basis” template where each supplier must fill in:
Then you compare total cost of ownership by adding operational risk considerations. Some organizations quantify this by estimating the cost of receiving delays, internal inspection labor, and potential rework. Others use qualitative risk tiers. Either approach is better than comparing raw unit prices without context.
You should also be cautious about “bait and switch” scope changes. Some suppliers provide a low initial quote but then add fees for documentation or revised inspection requirements. By forcing quote scope checklist completion, you reduce this risk. The key is to require that scope is stated upfront and that any changes are documented and approved before purchase order issuance.
Lead time commitments should align with your production schedule. If a supplier offers a shorter timeline, request a clear production plan and contingency assumptions (e.g., material availability and process scheduling).
It is helpful to require that suppliers describe lead time decomposition, such as:
If the supplier’s shorter lead time is achieved by skipping steps or reducing inspection scope, your total cost may rise. For example, expedited production can lead to insufficient measurement time, which increases the probability of acceptance failures. If certificates are generated later or with insufficient review time, documentation risk increases as well.
Also consider your receiving capabilities. If you schedule parts to arrive during a period when receiving staff is unavailable or your internal inspection workflow is overloaded, even an on-time shipment can become operationally late. Therefore, incorporate internal capacity and receiving windows into the schedule validation step.
On delivery, verify that labeling matches your inventory system, that certificates correspond to the correct batch, and that inspection reports align with the acceptance criteria agreed in the quote.
A receiving check should include a mapping between physical items, packaging labels, and documentation content. For parts tied to 33998412549, you should verify:
Receiving teams should also understand what constitutes a documentation rejection vs. a physical rejection. A documentation rejection might not mean the part is defective—it could mean it is not usable without traceability completion. To avoid confusion, define receiving disposition rules: what to quarantine, what to accept conditionally, and what to reject outright. This reduces internal delays and prevents “silent” acceptance of documentation that later becomes a compliance or audit risk.
If you have barcode scanning or ERP integration, confirm that the supplier’s label format supports your scanning workflow. If labels are missing, incorrectly positioned, or too small to scan reliably, you may create inventory reconciliation problems that slow production planning.
If nonconformance occurs, document containment actions and request a structured corrective action response. Evaluate effectiveness using evidence (e.g., reduced defect rate on follow-up batches or verified process adjustments).
Corrective action closure should include verification, not just planned changes. For example:
From a procurement perspective, corrective action also impacts future purchasing. If the supplier fails to provide timely closure evidence, you should reconsider your supplier score and purchasing volume. Over time, a disciplined approach creates an incentive structure where suppliers improve documentation and quality consistency—not just output.
Procurement and supplier-quality practices are widely discussed in operations and quality management literature. For instance, the quality management approach described in ISO 9001 emphasizes controlled processes, documentation, corrective actions, and continuous improvement—concepts that map directly to how buyers assess supplier readiness and manage risk. Similarly, ASQ (American Society for Quality) and other quality bodies publish guidance on inspection planning, root cause analysis, and quality system requirements that support consistent sourcing outcomes.
When evaluating suppliers, it is also common to refer to industry-neutral top practices around supplier audits and quality planning. These methods help reduce subjective decision-making and improve repeatability across procurement categories.
In practical terms, the ISO-aligned thinking is directly applicable to parts tied to 33998412549. If you treat your acceptance criteria as a controlled document with defined rules, you reduce variation in how different teams interpret requirements. If you treat your supplier’s certificate package as part of the controlled delivery process, you reduce the risk of receiving unusable shipments. If you treat nonconformance as an input to corrective action, you improve the system rather than just reacting to each incident.
Procurement is sometimes viewed as a transactional activity—quote, pay, receive. But in a well-run industrial environment, procurement is a system design activity. You are designing how the company interacts with suppliers to produce goods that meet specifications reliably. That design requires clarity on what constitutes conformity and what evidence proves conformity.
From a strategic standpoint, the “objective background” is therefore not just theoretical. It is the foundation of how organizations build supplier scorecards, reduce supply risk, and maintain compliance readiness over time. When the identifier 33998412549 is part of that controlled system, the documentation quality and traceability practices become part of your audit defensibility. That is why this article emphasizes aligning supplier capability and documentation quality before purchase.
In very supply-chain systems, a numeric identifier functions as a reference key to a specific part record, revision, or traceability entry. The number matters mainly because it should connect to verifiable technical documents such as drawings, material specs, and inspection/traceability records. Ask suppliers to confirm the exact record and revision they are quoting.
In practice, buyers should treat the identifier as a gateway to configuration control. Your procurement request should require suppliers to restate what revision/record they are referencing. That simple requirement often prevents “similar part” errors and ensures receiving can reconcile documentation correctly.
Differences usually come from scope and cost drivers such as material sourcing, machining complexity, finishing and heat-treatment steps, inspection intensity, documentation packages, lead-time scheduling, and packaging quality. A lower quote may reduce documentation or inspection scope, which can increase rework or receiving holds.
Another factor is risk pricing. Suppliers often price the possibility of nonconformance claims, rework, or quality disputes based on their past experience and their confidence in meeting your acceptance criteria. If one supplier has a more mature quality system or a more stable process, they may price less contingency. The buyer should avoid treating price differences as purely efficiency differences without checking scope and evidence.
Request representative inspection report formats, material certificates, traceability and labeling examples, and a brief description of how the supplier controls process changes. For higher criticality parts, consider requiring a pre-production sample with agreed acceptance criteria.
To make evidence requests more effective, explicitly define what “representative” means. For example, request certificates and inspection reports from a part with the same process route and similar tolerance/criticality level—not just any part the supplier has manufactured. If your part tied to 33998412549 requires specialized finishing or strict hardness control, request evidence from parts with those same critical characteristics.
Not automatically. Being nearby can reduce transit time and facilitate coordination, but reliability depends on manufacturing control, quality systems, documentation completeness, and whether the supplier can meet your acceptance criteria consistently.
Nearby sourcing can be beneficial for responsiveness to issues, but you still need a controlled process for verifying documents and traceability. Proximity does not ensure that certificates reference the correct revision, nor does it guarantee that labels include the correct identifier mapping for 33998412549.
Normalize quotes by scope: compare the same revision, the same deliverables (certificates and inspection scope), the same packaging requirements, and the same acceptance criteria. Then evaluate suppliers on both cost and risk factors such as traceability completeness and corrective action capability.
A fair comparison also requires consistent evaluation across internal stakeholders. Engineering might focus on specification compliance and critical-to-quality characteristics; quality assurance might focus on evidence completeness and control plans; warehouse receiving might focus on labeling and packaging compliance. Aligning these perspectives before awarding the purchase order prevents “surprise” mismatches later.
Use a pre-defined nonconformance workflow: contain affected lots, verify measurement results, document root cause analysis requests, and require evidence of corrective action effectiveness. Confirm that follow-up shipments address the identified failure mode.
Also define communication timelines. For example, set expectations on how quickly the supplier must respond to initial nonconformance reports, when they must provide containment and disposition, and when closure evidence must be submitted. Clear timelines reduce delays in deciding whether to continue using the supplier for other purchase orders tied to similar identifiers (including future variants of 33998412549 if applicable).
When sourcing industrial components tied to 33998412549, the strongest strategy is to treat supplier selection and price comparison as a structured risk-management process. Define scope and acceptance criteria first, demand evidence that supports traceability and quality control, and compare quotes on like-for-like terms. If you do this consistently—even when suppliers are “nearby”—you reduce surprises, protect production schedules, and build a more dependable supply base over time.
Ultimately, the number 33998412549 is not the value; it is the key that connects your purchase decision to configuration control, traceability, and proof of conformity. When you align supplier capability, documentation quality, and cost drivers before you purchase, you turn procurement from a transaction into a controlled process—one that protects both operational performance and compliance readiness.



This guide explains how 33998412549 and related sourcing details can inform procurement decisions, from verification to purchasing workflow. Objectively, numeric identifiers like 33998412549 are often used for traceability, catalog mapping, or internal stock references. The guide also clarifies what buyers should confirm with suppliers, including specifications, lead times, and documentation requirements.
This guide explains what the supplier reference 33998412549 typically signifies, how it functions in ordering and traceability, and what you should confirm with the supplier before approving goods. Objectively, supplier references support inventory matching, audit trails, and quality-control workflows across procurement and distribution.
This guide explains how to contact suppliers using 04569527728, how to structure your inquiry, and what to verify before you place an order. Objectively, keywords like supplier contact numbers support faster routing, clearer quoting, and smoother compliance checks. You’ll also find a comparison table of inquiry pathways and a step-by-step workflow to reduce miscommunication.
This guide explains how Texas Voucher programs are structured, what eligibility typically requires, and how families can evaluate participating options. Objectively, “Texas Voucher” refers to education-related funding mechanisms designed to support schooling choices, often with specific rules around providers, documentation, and student needs. The article also reviews practical steps to compare applications and compliance requirements.
This guide explains how Texas Voucher programs can affect school choice, costs, and compliance for families. It provides objective background on “Texas Voucher” policies, who administers related options, and what families typically evaluate when comparing eligible educational services. Readers will find conditions, practical steps, and common questions answered in an industry-focused tone.
This guide explains how Texas Voucher programs typically work, what families should verify, and how schools and suppliers handle eligibility and compliance. It provides objective background on voucher-style education funding, describes practical decision points, and outlines common requirements and risks to consider—helping readers evaluate options with care.
This guide explains how Texas Voucher programs work, what families should evaluate, and how to compare options responsibly. It provides objective background on vouchers in education, including typical eligibility considerations, program design factors, and due-diligence steps. Designed for readers seeking clear, practical insight into planning decisions near the Texas education landscape.
This guide explains how Texas Voucher programs work, what families should verify, and how to evaluate eligibility and provider requirements. It offers objective background on voucher-style education funding, the policy goals behind school choice, and the due diligence steps families can use before enrollment decisions.